The High-Stakes Physics of Hardware Commercialization
\n
In software engineering, the cost of iterating on code is infinitesimally low: a developer modifies a few lines of syntax, runs automated unit tests, and deploys a hotfix to cloud servers within minutes. Hardware development, by contrast, obeys the unyielding laws of physical chemistry, metallurgy, thermodynamics, and expensive industrial capital. When an injection mold tool for a complex consumer enclosure is cut from P20 hardened steel at a cost of $250,000, a dimensional drafting error of half a millimeter cannot be corrected with an over-the-air firmware update. It results in scrapped tooling, months of supply chain delays, and catastrophic capital destruction.
To navigate this brutal reality, industrial manufacturing organizations rely on the Stage-Gate Product Development Framework. Pioneered by Dr. Robert G. Cooper in the 1980s and refined over four decades by global hardware leaders such as General Electric, Apple, Sony, and Medtronic, the Stage-Gate system is an operational and managerial blueprint that decomposes the chaotic journey from napkin sketch to mass manufacturing into discrete, sequential stages punctuated by rigorous decision-making gates.
Each gate acts as a quantitative tollbooth where cross-functional executives—representing industrial design, mechanical engineering, electrical engineering, quality assurance, finance, and procurement—interrogate project deliverables against unforgiving criteria: technical feasibility, tooling ROI, regulatory compliance, and unit economic margins. In this comprehensive engineering guide, we deconstruct every phase of the hardware commercialization pipeline, examining Phase 0 discovery, architecture freeze, the EVT/DVT/PVT validation gauntlet, and mass production ramp.
\n
⚙️ The Golden Axiom of Hardware Engineering: The Rule of Tens
‘A defect that costs $1 to catch on the concept sketch costs $10 to fix in CAD, $100 to correct during prototyping, $1,000 to resolve in pre-production tooling, and $10,000 to remediate after one hundred thousand units have been shipped to global retail shelves.’ — The Rule of Tens underpins the entire Stage-Gate discipline.
\n
Phase 0: Ideation, Market Validation, and Product Requirements (PRD)
\n
Every commercial hardware product begins in the discovery funnel: identifying latent customer friction points, technological breakthroughs, or market vulnerabilities. However, unconstrained ideation without structured engineering constraints is the primary root cause of scope creep and fatal budget overruns. Phase 0 exists to transform nebulous inspiration into a concrete, legally binding engineering contract: the Product Requirements Document (PRD).
A masterclass PRD bridges the divide between marketing aspirations and physical mechanics. It specifies not merely what the product should feel like, but precisely quantified physical parameters:
- Form Factor and Envelope: Bounding box dimensions (length, width, height in millimeters), total target mass (grams), and ergonomic center-of-gravity constraints.
- Environmental Operating Envelope: Operating temperature ranges (-20°C to +60°C), ingress protection ratings (e.g., IP68 water and dust submersion), UV resistance tolerances, and drop impact survival specifications (e.g., survivability from 1.5 meters onto hard concrete).
- Electrical and Acoustic Performance: Battery operating life under defined workload duty cycles, thermal dissipation wattage, peak wireless transmission wattage (Wi-Fi, Bluetooth, cellular), and maximum allowable fan acoustic noise in decibels (dBA).
- Cost Targets (Target BoM): Strict limits on the total Bill of Materials (BoM) cost to guarantee sustainable retail gross margins (typically demanding a 3.5x to 4x multiplier between BoM cost and Manufacturer’s Suggested Retail Price / MSRP).
Gate 0 approval represents the formal commitment of exploratory research funding, authorizing cross-functional teams to initiate preliminary industrial styling and mechanical feasibility architecture.
\n
| Development Milestone | Primary Engineering Focus | Typical Build Quantity | Tooling Status | Key Exit Deliverable |
|---|---|---|---|---|
| Phase 0: Discovery & PRD | Market need, target BoM, regulatory scope | 0 units (CAD & foam models) | No tooling authorized | Signed off PRD & preliminary financial model |
| Phase 1: Concept & Architecture | ID concepts, PCB form-factor, mechanical layout | 5 – 15 functional mockups | Soft 3D printing & CNC machining | Approved ID clay/CAD freeze & architectural schematics |
| EVT (Engineering Validation) | Core functional verification, signal integrity | 20 – 100 prototype units | Soft prototype tooling (silicone/aluminum) | Proof that all core subsystem electronics & mechanics function |
| DVT (Design Validation) | Cosmetics, final materials, drop/climatic testing | 100 – 500 pre-pilot units | Hard production steel tooling (P20/H13) | Verification that production tooling meets all cosmetic & reliability specs |
| PVT (Production Validation) | Line balance, cycle times, yield optimization | 500 – 2,000 pilot units | Final multi-cavity steel molds at full speed | Attainment of >98% first-pass production line yield |
| Mass Production (MP) | Continuous automated manufacturing & logistics | 10,000 – 1,000,000+ units | Full factory automation & robotic fixtures | Full commercial retail availability & ongoing SPC monitoring |
\n
Phase 1: Concept Development and Architecture Freeze
\n
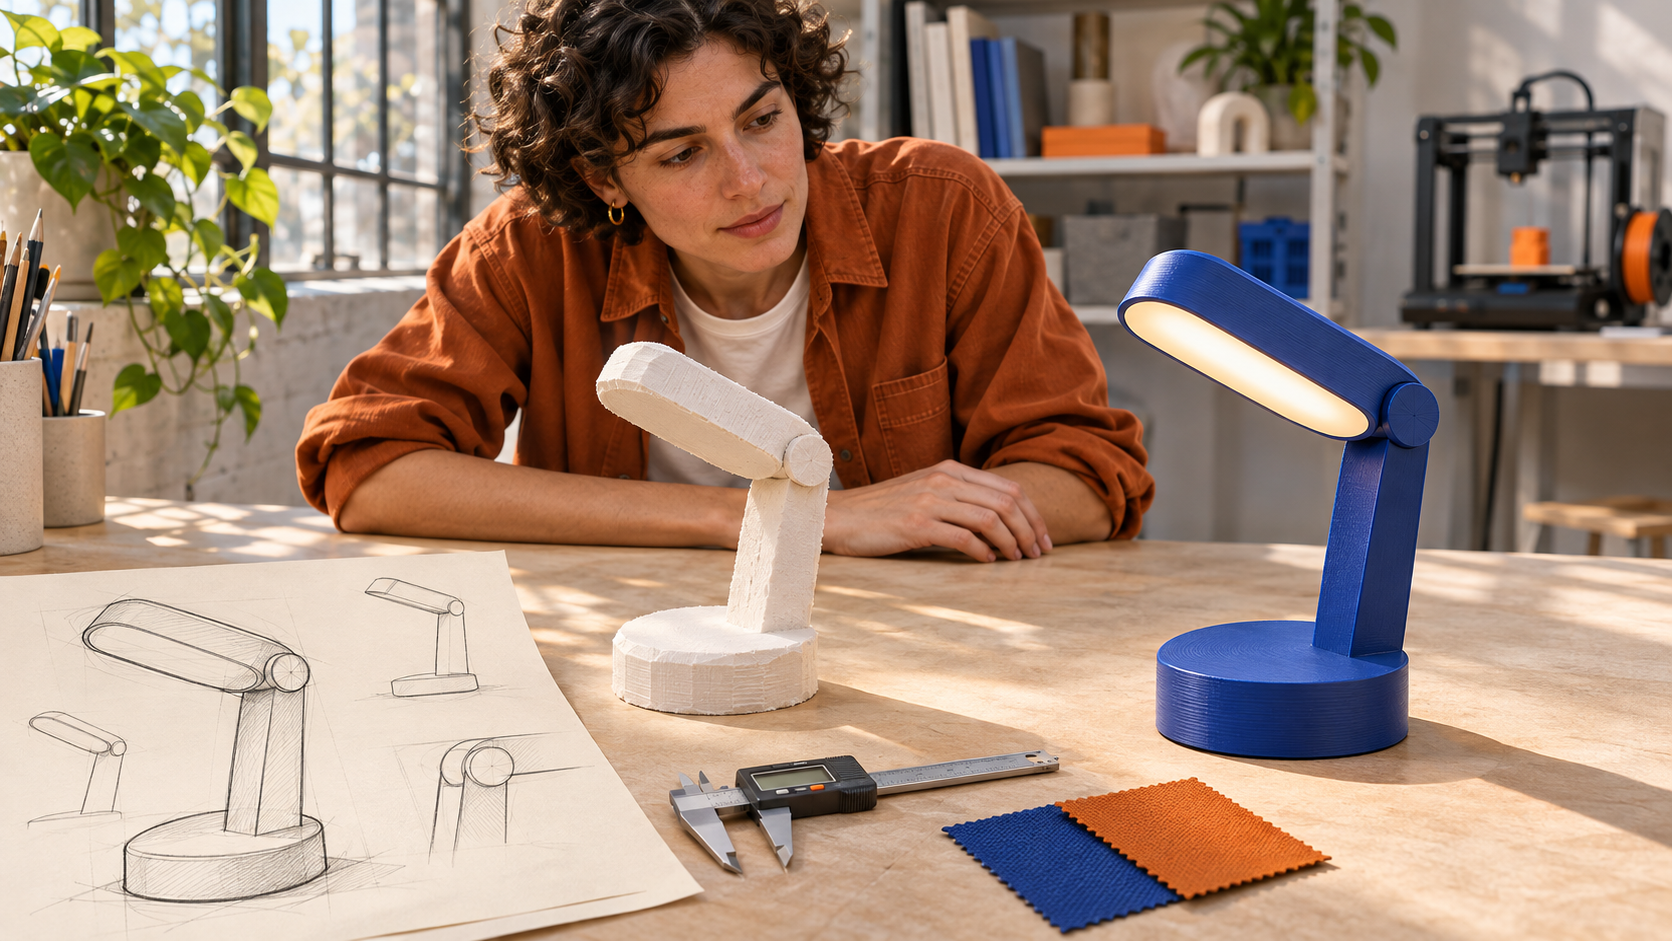
Once Gate 0 is crossed, industrial designers (ID) and mechanical engineers (ME) initiate an intense collaborative sprint. Industrial designers explore aesthetic form factors, user ergonomics, material finishes, and brand semantics through hundreds of 2D concept sketches and 1:1 scale polyurethane foam prototypes. Simultaneously, mechanical and electrical systems architects map out the internal spatial layout: battery placement, Printed Circuit Board (PCB) geometry, antenna keep-out zones, heat sinks, and structural chassis ribs.
This phase is fraught with creative tension between ID and ME teams. Industrial designers naturally seek the thinnest possible profile, sweeping curvature, and minimal seam gaps. Mechanical engineers must advocate for sufficient wall thickness (typically 1.5 to 2.5 mm in injection-molded thermoplastics to prevent short shots and sink marks), structural draft angles, shock-absorption clearance for lithium-ion battery swelling, and adequate copper trace clearance for RF antenna radiation efficiency.
The culmination of Phase 1 is the Architecture Freeze (also known as the Industrial Design Freeze). High-precision high-density CNC appearance models are milled from block ABS or aluminum, painted to production color/finish standards, and evaluated by leadership. Passing Gate 1 locks the external cosmetic surfaces (A-surfaces), allowing tooling engineers and electrical layout teams to begin formal production-intent detailed design.
\n
Phase 2: EVT (Engineering Validation Test) — Proving the Physics
\n
With external styling locked, the program enters the unforgiving crucible of the three-letter validation gauntlet: EVT, DVT, and PVT. The first of these is the Engineering Validation Test (EVT).
The fundamental mission of EVT is simple yet merciless: Does the integrated system work as a functional physical instrument? EVT units (typically 20 to 100 builds) are assembled using production-intent electronic circuit boards (motherboards, sensor flexes, power supplies) housed within early prototype mechanical enclosures. These enclosures are often fabricated via high-precision stereolithography (SLA), selective laser sintering (SLS), or rapid aluminum prototype tooling rather than final production hardened steel molds.
During EVT, test engineers execute exhaustive battery run-time tests, thermal imaging scans under full CPU/GPU loads to identify component hot spots, signal integrity audits on high-speed data buses, and antenna chamber measurements (Passive and Active Over-the-Air / OTA testing) inside anechoic chambers to confirm RF gain and efficiency. If a critical thermal dissipation bottleneck or electromagnetic interference (EMI) loop is discovered during EVT, the mechanical layout can still be altered without destroying millions of dollars in production tooling. Passing Gate 2 requires zero unresolved catastrophic electrical or mechanical architecture bugs.
\n
⚡ EVT Insight: The Silicon & Copper Reality Check
EVT is where theoretical simulations meet real-world parasitic inductance, thermal resistance, and material flexing. A CAD model may show zero clearance conflicts, but when physical components are populated on a PCB, solder reflow tolerances, thermal expansion coefficients, and connector insertion forces quickly expose hidden structural weaknesses.
\n
Phase 3: DVT (Design Validation Test) — Proving the Tooling and Environment
\n
Passing EVT unlocks the most capital-intensive milestone in the product lifecycle: the authorization to cut Hard Production Tooling. Steel injection molds, sheet metal stamping dies, die-casting tools, and automated assembly fixtures are commissioned from specialized toolmakers. The project advances into Design Validation Test (DVT).
DVT units (typically 100 to 500 units) are the first devices assembled entirely from production-intent materials manufactured on production-intent tooling. Polycarbonate enclosures come out of actual hardened steel mold cavities with final Mold-Tech textures; magnesium sub-frames are high-pressure die-cast; custom silicone seals are compression molded. The primary question of DVT shifts from ‘Does the design work?’ to ‘Does our production tooling produce parts that meet every cosmetic, dimensional, and environmental reliability standard?’
DVT is characterized by brutal, destructive environmental and reliability qualification testing (often referred to as HALT/HASS testing):
- Thermal Shock and Cycling: Placing units in environmental chambers cycling rapidly between -40°C and +85°C over hundreds of hours to induce fatigue failure in solder joints and differential thermal expansion cracks.
- Tumble and Drop Gauntlet: Subjecting devices to repeated falls from varying heights onto steel plates and concrete surfaces using automated pneumatic drop towers, verified by high-speed video recording at 10,000 frames per second.
- Ingress and Fluid Exposure: Blasting enclosures with high-pressure water jets, salt-fog corrosion sprays (ASTM B117), synthetic human sweat, cosmetic lotions, and abrasive particulate dust.
- Actuator Cycle Durability: Pneumatic robotic fingers pressing mechanical pushbuttons, rotating knobs, and flexing USB-C ports through 50,000 to 100,000 continuous cycles to confirm switch contact resistance and tactile detent retention.
Simultaneously, DVT units are submitted to accredited government regulatory laboratories worldwide to achieve mandatory legal certifications: FCC (United States), CE (European Union), UL (Underwriters Laboratories safety certification), RoHS (hazardous substance compliance), and WEEE.
\n
Phase 4: PVT (Production Validation Test) — Proving the Factory Line
\n
Once DVT proves that the product survives real-world abuse and satisfies global regulatory mandates, one final hurdle remains before commercial release: the factory floor itself. This is the realm of Production Validation Test (PVT).
A flawless product design is useless if the contract manufacturer’s assembly line cannot build it quickly, repeatably, and profitably. PVT builds (typically 500 to 2,000 units) are run at the contract manufacturing facility at full target production line speed. The focus of PVT is not the product itself, but the optimization of manufacturing operational metrics:
- First Pass Yield (FPY): The percentage of manufactured units that pass every single automated optical inspection (AOI), in-circuit test (ICT), and functional test station without requiring manual rework or component scrapping (world-class consumer electronics lines target FPY > 98%).
- Takt Time and Line Balancing: Measuring the exact cycle time in seconds at each assembly station—from automated screw driving and adhesive dispensing to final packaging—eliminating worker bottlenecks to match factory throughput to market demand.
- Statistical Process Control (SPC): Tracking critical-to-quality (CTQ) physical dimensions using automated coordinate measuring machines (CMM) to verify that process capability metrics ($C_{pk}$) remain strictly above 1.33, guaranteeing that part variances conform to normal distribution tolerances.
- Work Instruction Optimization: Refining step-by-step Standard Operating Procedures (SOPs) with visual pictorial guides to eliminate operator assembly errors and fatigue.
Crucially, units produced during a successful PVT run that pass all quality criteria are not scrapped—they are packaged in retail boxes and become the first commercial revenue units shipped to global distribution warehouses.
\n
Phase 5: Mass Production (MP) Ramp and Sustaining Engineering
\n
With Gate 4 formally cleared, the green flag drops for Mass Production (MP) Ramp. Production volumes scale exponentially: from 5,000 units per week to 50,000 or 500,000 units per week. However, the product development lifecycle does not conclude when the factory reaches maximum speed; it transitions into Sustaining Engineering.
Sustaining engineering teams monitor real-world customer return rates (Return Merchandise Authorization / RMA data), tracking failure Pareto charts to identify emerging reliability trends. If field returns reveal an unexpected solder joint fatigue or component degradation from a secondary component supplier, sustaining engineers execute root-cause analyses, issue Engineering Change Orders (ECOs), and adjust assembly line torque settings or adhesive curing times. Sustaining teams also manage Value Engineering (VE) initiatives—identifying opportunities to reduce Bill of Materials costs, consolidate sub-components, or negotiate raw material volume discounts without compromising product quality.
\n
Contract Manufacturing Dynamics: OEM, ODM, and JDM Engagement Models
\n
A flawless Stage-Gate process within corporate headquarters is meaningless without the industrial execution of a Contract Manufacturer (CM). Hardware organizations must navigate three distinct commercial engagement models:
- Original Equipment Manufacturer (OEM): The brand owns 100% of the intellectual property, industrial design, mechanical CAD, electrical schematics, and firmware. The brand pays Non-Recurring Engineering (NRE) tooling costs and owns every injection mold and stamping die. The contract manufacturer (Tier 1 giants like Foxconn, Flex, Jabil, or Celestica) simply provides factory floor labor, surface-mount technology (SMT) lines, and logistics assembly. This model affords maximum quality control but requires immense internal engineering bandwidth.
- Original Design Manufacturer (ODM): The manufacturer already owns a pre-developed ‘white-label’ hardware platform (common in monitors, electric kettles, and power supplies). The brand merely applies cosmetic branding, logo badging, and customized packaging. While time-to-market is rapid and development capital is minimal, the brand has zero IP ownership, cannot differentiate hardware features, and suffers razor-thin gross profit margins.
- Joint Design Manufacturer (JDM): A hybrid co-development model where the brand defines the industrial design, user experience, and core PRD, while the offshore manufacturer’s engineering staff develops the detailed internal mechanical ribs, PCB trace routing, and local component sourcing. The JDM model accelerates engineering velocity but requires stringent legal contracts to safeguard proprietary trade secrets and tooling asset rights.
During EVT, DVT, and PVT builds, top-tier hardware companies send multidisciplinary engineering fly-in teams directly to offshore factory floors. Living in local hotels adjacent to the manufacturing plant for weeks at a time, these ‘factory floor warriors’ work 16-hour shifts directly alongside line operators: debugging surface-mount solder defects, fine-tuning robotic screw-driving torques, and resolving tooling injection issues in real time. This intimate physical presence on the line is often the singular difference between a triumphant product launch and an embarrassing six-month delay.
\n
Conclusion: The Discipline of Physical Creation
\n
The Stage-Gate Product Development Framework is the ultimate antidote to corporate wishful thinking in hardware engineering. It enforces an uncompromising culture of empirical truth: demanding physical prototypes rather than optimistic PowerPoint slides, rigorous reliability test data rather than subjective opinions, and statistical manufacturing capability rather than blind faith.
Mastering this disciplined pipeline transforms hardware creation from an unpredictable, financially hazardous gamble into a repeatable, scalable engine of industrial innovation. By respecting the immutable physics of physical manufacturing and shepherding complex ideas through the methodical gates of EVT, DVT, and PVT, engineering organizations earn the supreme privilege of delivering reliable, beautiful, and transformative products into the hands of millions worldwide.