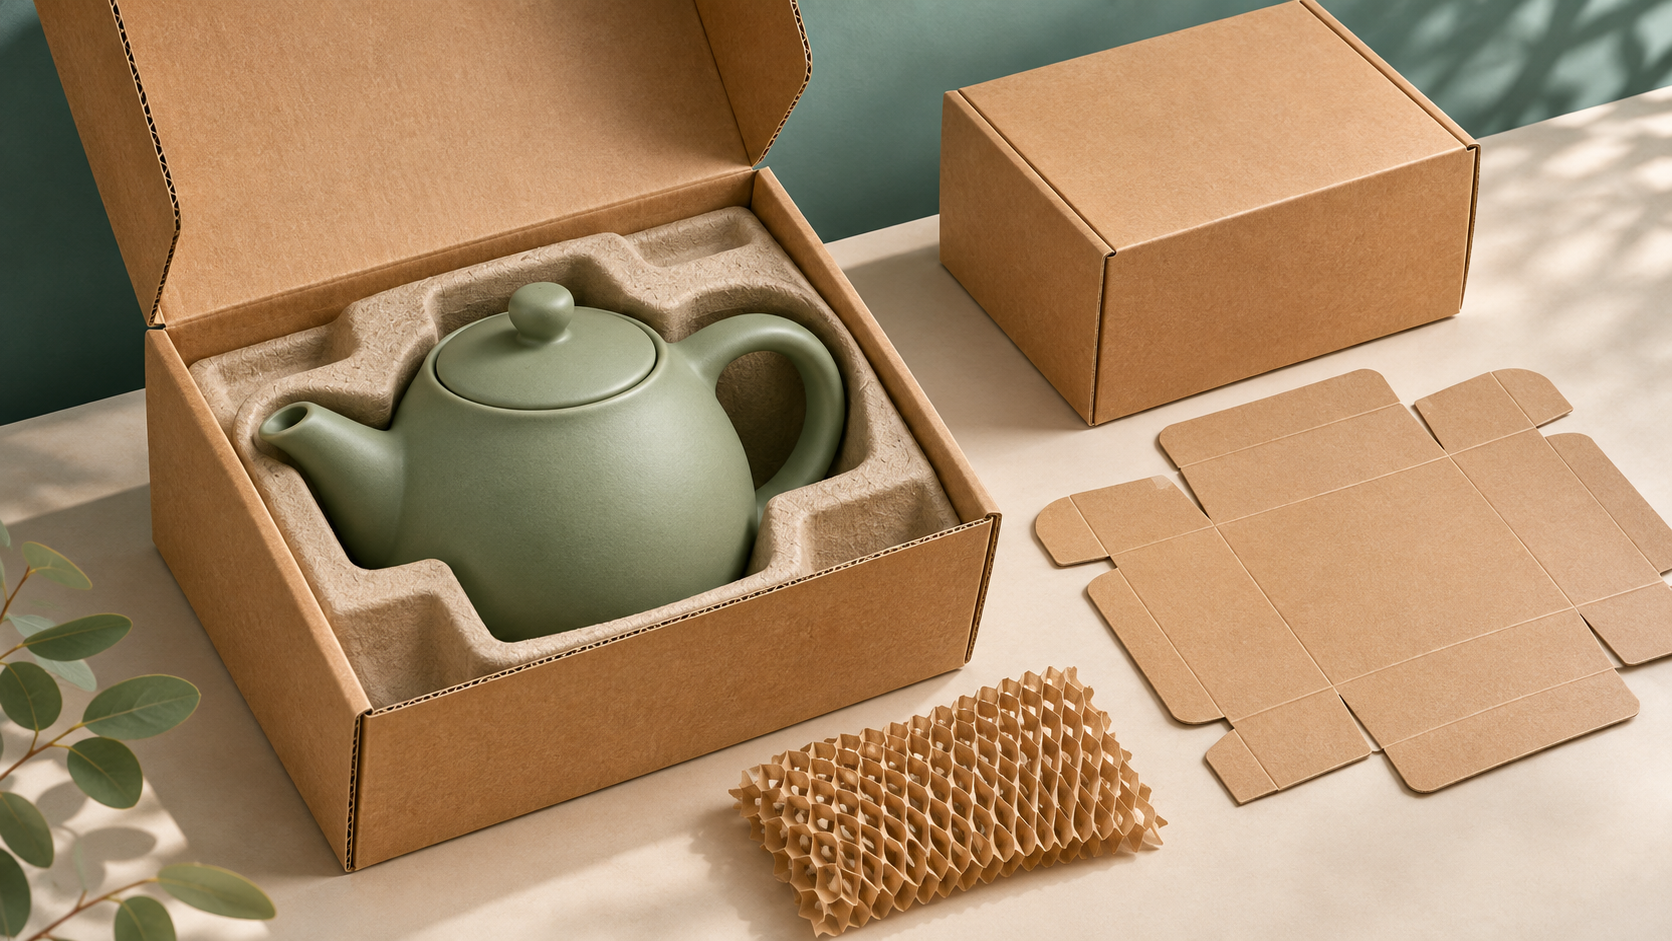
The Invisible Engineering Shield of Global Commerce
\n
Every single day, across the planetary logistics arteries of global commerce, billions of commercial products journey through an unforgiving, chaotic physical gauntlet. Pallets stacked three meters high are hoisted by roaring diesel forklifts, tossed inside intermodal shipping containers traversing tempestuous oceans, jolted across rail freight switches, bounced over potholed arterial highways, and hurled onto high-speed sorting conveyors inside automated fulfillment fulfillment centers. Throughout this brutal kinematic journey, the sole barrier standing between an expensive, delicate consumer product and catastrophic physical destruction is an artifact often dismissed as mundane trash: Engineered Packaging.
Far from being a mere paper box or cosmetic container, modern protective packaging is a sophisticated discipline of civil and mechanical engineering executed in cellulose fiber and polymer geometry. Structural packaging engineering combines classical beam mechanics, structural acoustics, material rheology, and finite element impact modeling to design lightweight, high-strength protective enclosures capable of surviving immense static compression, dynamic harmonic vibration, and high-velocity kinematic drop impacts while minimizing material volume and shipping freight costs.
In this comprehensive engineering treatise, we deconstruct the physics and manufacturing mechanics of structural packaging: analyzing the micro-mechanics of corrugated flute profiles, the precision tooling of flatbed and rotary die-cutting, the mathematical calculation of compressive box strength via the McKee Formula, and the rigorous international transit qualification protocols codified under ASTM and ISTA standards.
\n
📦 The Core Axiom of Packaging Engineering
‘Under-packaging results in damaged products, costly reverse logistics, and destroyed brand reputation. Over-packaging wastes billions of dollars in excess freight, consumes unnecessary planetary resources, and creates consumer rage. The objective of the packaging engineer is the mathematically optimal threshold: maximum physical protection with minimum material mass.’
\n
The Architecture of Corrugated Board: Fluting Geometry and Beam Mechanics
\n
The undisputed workhorse of global transport packaging is Corrugated Fiberboard, patented in the nineteenth century for reinforcing top hats and transformed by the mid-twentieth century into the foundational structural substrate of global supply chains. At the mechanical level, corrugated fiberboard functions identically to an architectural I-beam or an engineered truss bridge.
A standard corrugated sheet consists of two flat outer paper facings—known as Linerboards (typically fabricated from unbleached virgin Kraft pulp made via the sulfate chemical pulping process for maximum tensile strength)—sandwiching an undulating, wave-like core known as the Corrugated Medium (Fluting) (often fabricated from semi-chemical hardwood pulp or 100% recycled fiber). When the undulating medium is adhesive-bonded to the liners using heated cornstarch adhesives, the resulting composite structure achieves an astonishing stiffness-to-weight ratio: the flat liners resist bending tensile and compressive stresses, while the fluted medium acts as a continuous web that resists shear deformation and prevents the liners from buckling inward under perpendicular load.
Packaging engineers specify corrugated board based on standardized Flute Profiles, each optimized for distinct mechanical duty cycles:
- A-Flute (~4.8 mm thickness, ~105 flutes/meter): The thickest standard single-wall profile. Provides supreme cushioning capacity and high vertical stacking compression strength, making it ideal for fragile, heavy industrial machinery.
- B-Flute (~3.2 mm thickness, ~150 flutes/meter): Characterized by higher flute density. Offers exceptional crush resistance, puncture resistance, and a flatter surface profile that accepts high-quality flexographic ink printing, commonly used for retail canned goods and die-cut self-locking mailers.
- C-Flute (~4.0 mm thickness, ~128 flutes/meter): The universal compromise between A and B flutes. Represents over 80% of all standard shipping boxes (RSC – Regular Slotted Cartons) worldwide, providing balanced compression stacking and puncture protection.
- E-Flute (~1.6 mm thickness, ~295 flutes/meter) & Micro-Flutes (F, N): Ultra-thin fluting engineered to displace rigid folding cartons. Delivers exceptional crush resistance and photographic printability, serving as the industry standard for high-end consumer electronics packaging, small cosmetics, and retail hardware displays.
- Double-Wall & Triple-Wall Combinations (e.g., BC-Flute ~7.0 mm, AAC-Flute ~15 mm): Combining multiple fluting profiles into heavy-duty laminated sheets capable of carrying over 1,000 kilograms of bulk chemicals or automotive engine blocks, replacing heavy wooden shipping crates.
\n
| Flute Profile | Nominal Thickness | Flutes per Linear Meter | Primary Mechanical Strength | Dominant Industrial Application |
|---|---|---|---|---|
| A-Flute | 4.8 mm (3/16 in) | ~105 – 110 flutes/m | Supreme vertical stacking & shock absorption | Heavy fragile goods, glass carboys, delicate instrumentation |
| B-Flute | 3.2 mm (1/8 in) | ~145 – 155 flutes/m | High flat-crush resistance & puncture resistance | Die-cut mailer boxes, canned goods trays, retail food packaging |
| C-Flute | 4.0 mm (5/32 in) | ~125 – 135 flutes/m | Balanced stacking compression & impact resistance | Universal standard Regular Slotted Cartons (RSC shipping boxes) |
| E-Flute | 1.6 mm (1/16 in) | ~290 – 310 flutes/m | Superior surface flatness & print fidelity | Consumer electronics retail boxes, luxury cosmetics, shoe boxes |
| BC Double-Wall | 7.0 mm (9/32 in) | Combined B + C layers | Extreme puncture resistance & heavy load stacking | Major domestic appliances (refrigerators, washers), bulk chemicals |
\n
The Mathematics of Stacking: The McKee Formula and Edge Crush Testing (ECT)
\n
In modern high-density automated warehouses, pallets loaded with corrugated boxes are stacked five to six levels high for months under varying ambient humidity and temperatures. If the bottom box buckles under compressive load, the entire pallet stack collapses, resulting in catastrophic loss. Packaging engineers do not guess whether a box will survive; they calculate its ultimate Box Compression Strength (BCT) using mathematical failure mechanics.
Historically, the industry measured board quality via the Mullen Burst Test (bursting pressure in pounds per square inch / psi). However, burst strength only measures puncture resistance; it has virtually zero mathematical correlation with how much weight a box can support vertically in a warehouse stack. Modern engineering relies on the Edge Crush Test (ECT), codified under TAPPI T 811. ECT measures the maximum edgewise compressive force a short column of corrugated board can sustain parallel to the flutes before crushing, expressed in kilonewtons per meter (kN/m) or pounds per linear inch (pli).
In 1963, R.C. McKee and his research team at the Institute of Paper Chemistry derived the famous McKee Formula, which relates a box’s physical dimensions and board properties to its theoretical top-to-bottom compression strength:
$$\text{BCT} = 5.876 \times \text{ECT} \times \sqrt{T \times P}$$
Where:
- BCT: Theoretical Box Compression Test strength in Newtons (or pounds force).
- ECT: Edge Crush Test value of the board in kN/m (or lb/in).
- T: Caliper thickness of the corrugated board sheet in millimeters (or inches).
- P: Internal perimeter of the box base ($P = 2 \times [\text{Length} + \text{Width}]$).
However, theoretical laboratory BCT reflects pristine conditions (23°C at 50% relative humidity with perfectly distributed vertical loads). In real-world logistics, packaging engineers must apply a stringent Safety Factor ($SF$)—typically ranging from 3.0 to 5.0—to account for environmental degradation: high ambient humidity (which softens cellulose hydrogen bonds, reducing box strength by up to 50% at 90% RH), pallet overhang (a 1-inch box overhang beyond the wooden pallet edge degrades compression capacity by 30%), dynamic truck transit vibration, and warehouse storage duration.
\n
⚠️ The Deadly Impact of Pallet Overhang
A corrugated shipping container achieves over 60% of its vertical compressive stacking strength directly from its four vertical folded corners. When a pallet is improperly stacked so that the box edges overhang the wooden pallet deck by just 25 mm, the load-bearing vertical corners lose their solid baseline support, causing the box’s effective compression capacity to collapse by up to 32% instantly.
\n
Precision Manufacturing: Die-Cutting Tooling and Folding Geometry
\n
Transforming flat corrugated sheets into functional three-dimensional packaging structures requires high-speed industrial die-cutting. Packaging manufacturing relies on two dominant technological methodologies:
- Flatbed Die-Cutting: A reciprocating hydraulic or mechanical press drives a flat, laser-cut high-density plywood die board (typically 18 mm thick) perpendicularly down onto a corrugated sheet resting on a hardened steel counter-plate. Embedded in the wood die are precision steel cutting rules (ground with razor-sharp beveled edges to slice cleanly through fibers) and scoring/creasing rules (rounded, blunted steel blades that compress the fluting without cutting, forming crisp, accurate fold hinges). Flatbed die-cutting provides supreme dimensional accuracy (+/- 0.2 mm), tight tolerances, and sharp crease lines, making it the undisputed standard for intricate consumer electronics packaging, display cartons, and complex internal folded inserts.
- Rotary Die-Cutting: Utilizes two counter-rotating cylinders: an upper steel cylinder carrying curved wooden or flexible magnetic die plates, and a lower anvil cylinder covered in resilient polyurethane blankets. Flat corrugated sheets are fed through the nip at blistering speeds exceeding 300 to 500 meters per minute. While rotary die-cutting has slightly looser dimensional tolerances ($\pm 1.0$ mm) due to cylinder radius curvature and blanket wear, its sheer throughput makes it the dominant manufacturing engine for high-volume corrugated shipping cartons.
Structural packaging designers utilize specialized CAD suites (such as ArtiosCAD or Impact) to engineer intricate folded geometries that eliminate adhesives entirely. Self-locking designs—such as the iconic Roll End Tuck Front (RETF) mailer, crash-lock auto-bottom cartons, and snap-lock bottoms—utilize interlocking tabs, friction-fit side flaps, and double-wall folding sides to achieve tremendous torsional rigidity and tamper-evident security without requiring a single drop of hot-melt glue or packaging tape.
\n
Cushioning Mechanics: Shock Curves and Fragility Analysis
\n
When an packaged electronic product—such as a television, a laser printer, or a high-end coffee espresso machine—is dropped onto concrete, the outer box strikes the floor and comes to an instantaneous halt. However, the delicate internal payload continues to move downward at velocity until arrested by the internal cushioning material. If the cushioning is too stiff, the deceleration shock pulse ($G$-force) transmitted to the payload will shatter internal circuit boards or dislodge optical lenses. If the cushioning is too soft, the payload will compress the cushion completely (‘bottom out’), experiencing a catastrophic shock spike.
Packaging engineers utilize Shock and Fragility Analysis to engineer the internal protective suspension:
- Product Fragility Rating ($G_{crit}$): Determined via drop-table shock testing under ASTM D3332. Fragility represents the maximum peak deceleration shock (expressed in multiples of gravitational acceleration, $G$) that the unpackaged product can withstand without sustaining functional or cosmetic damage (e.g., a rugged power drill can survive $80G$, whereas a delicate medical spectrometer will be destroyed at $25G$).
- Dynamic Cushioning Curves: Material testing laboratories generate empirical Cushion Curves (ASTM D1596) for various packaging foams (Expanded Polyethylene / EPE, Expanded Polypropylene / EPP, molded pulp, and corrugated partitions). A cushion curve plots transmitted peak acceleration ($G$) versus static loading pressure ($ ext{psi}$ or $ ext{kPa}$) for a given drop height (typically 30 to 48 inches) and cushion thickness (e.g., 25 mm, 50 mm, 75 mm).
- Operating Cushion Window: The engineer calculates the static loading of the product ($W / A$, where $W$ is payload weight and $A$ is cushion bearing surface area) and selects a foam thickness and density where the transmitted $G$-force on the curve remains safely below the product’s $G_{crit}$ threshold across all anticipated drop heights.
\n
The Transit Gauntlet: ASTM D4169 and ISTA Testing Protocols
\n
To verify that an engineered packaging system will protect its contents throughout global distribution, prototypes are subjected to international transit simulation standards, most notably ASTM D4169 (Standard Practice for Performance Testing of Shipping Containers and Systems) and ISTA (International Safe Transit Association) Series 2 and 3 protocols.
These laboratory protocols replicate the physical hazards of transport under controlled, repeatable conditions:
- Free-Fall Drop Testing: The packaged product is mounted in a pneumatic drop-leaf release fixture and dropped from specified heights (e.g., 76 cm to 120 cm depending on package mass) onto a 10-ton flat steel and concrete floor in a strict 10-drop sequence: one drop onto the most fragile corner, three drops onto the edges radiating from that corner, and six drops onto all flat faces.
- Random Multi-Axis Vibration Testing: The package is secured to an electrodynamic or hydraulic shake table programmed with real-world Power Spectral Density (PSD) vibration profiles recorded from actual long-haul tractor-trailers, cargo aircraft, and freight trains (spanning 1 Hz to 200 Hz for several hours). This tests for fastener loosening, component scuffing, and fatigue failure caused by harmonic resonance.
- Compressive Warehouse Simulation: The box is placed inside a hydraulic compression platens machine and subjected to sustained compressive loads equivalent to five times the calculated stack weight under 38°C and 85% relative humidity for 72 continuous hours.
- Atmospheric Low-Pressure Altitude Testing: Packaged goods destined for air freight are placed in vacuum decompression chambers simulating 14,000 feet altitude (hypobaric conditions) to verify that sealed internal pouches and bottles do not burst or leak due to internal air expansion.
\n
Conclusion: The High Art of Protective Packaging
\n
Structural packaging engineering is the unsung hero of modern technological civilization. It allows the breathtaking innovations of silicon foundries, precision optics laboratories, and automated manufacturing lines to cross oceans and continents unharmed, arriving in the hands of the end-user in pristine operational condition.
By mastering the geometric mechanics of corrugated flutes, the predictive mathematics of the McKee formula, the fluid dynamics of die-cutting tooling, and the merciless rigor of ISTA transit simulations, packaging engineers construct lightweight, sustainable, and impenetrable physical shields that empower the global economy to function with breathtaking efficiency and reliability.